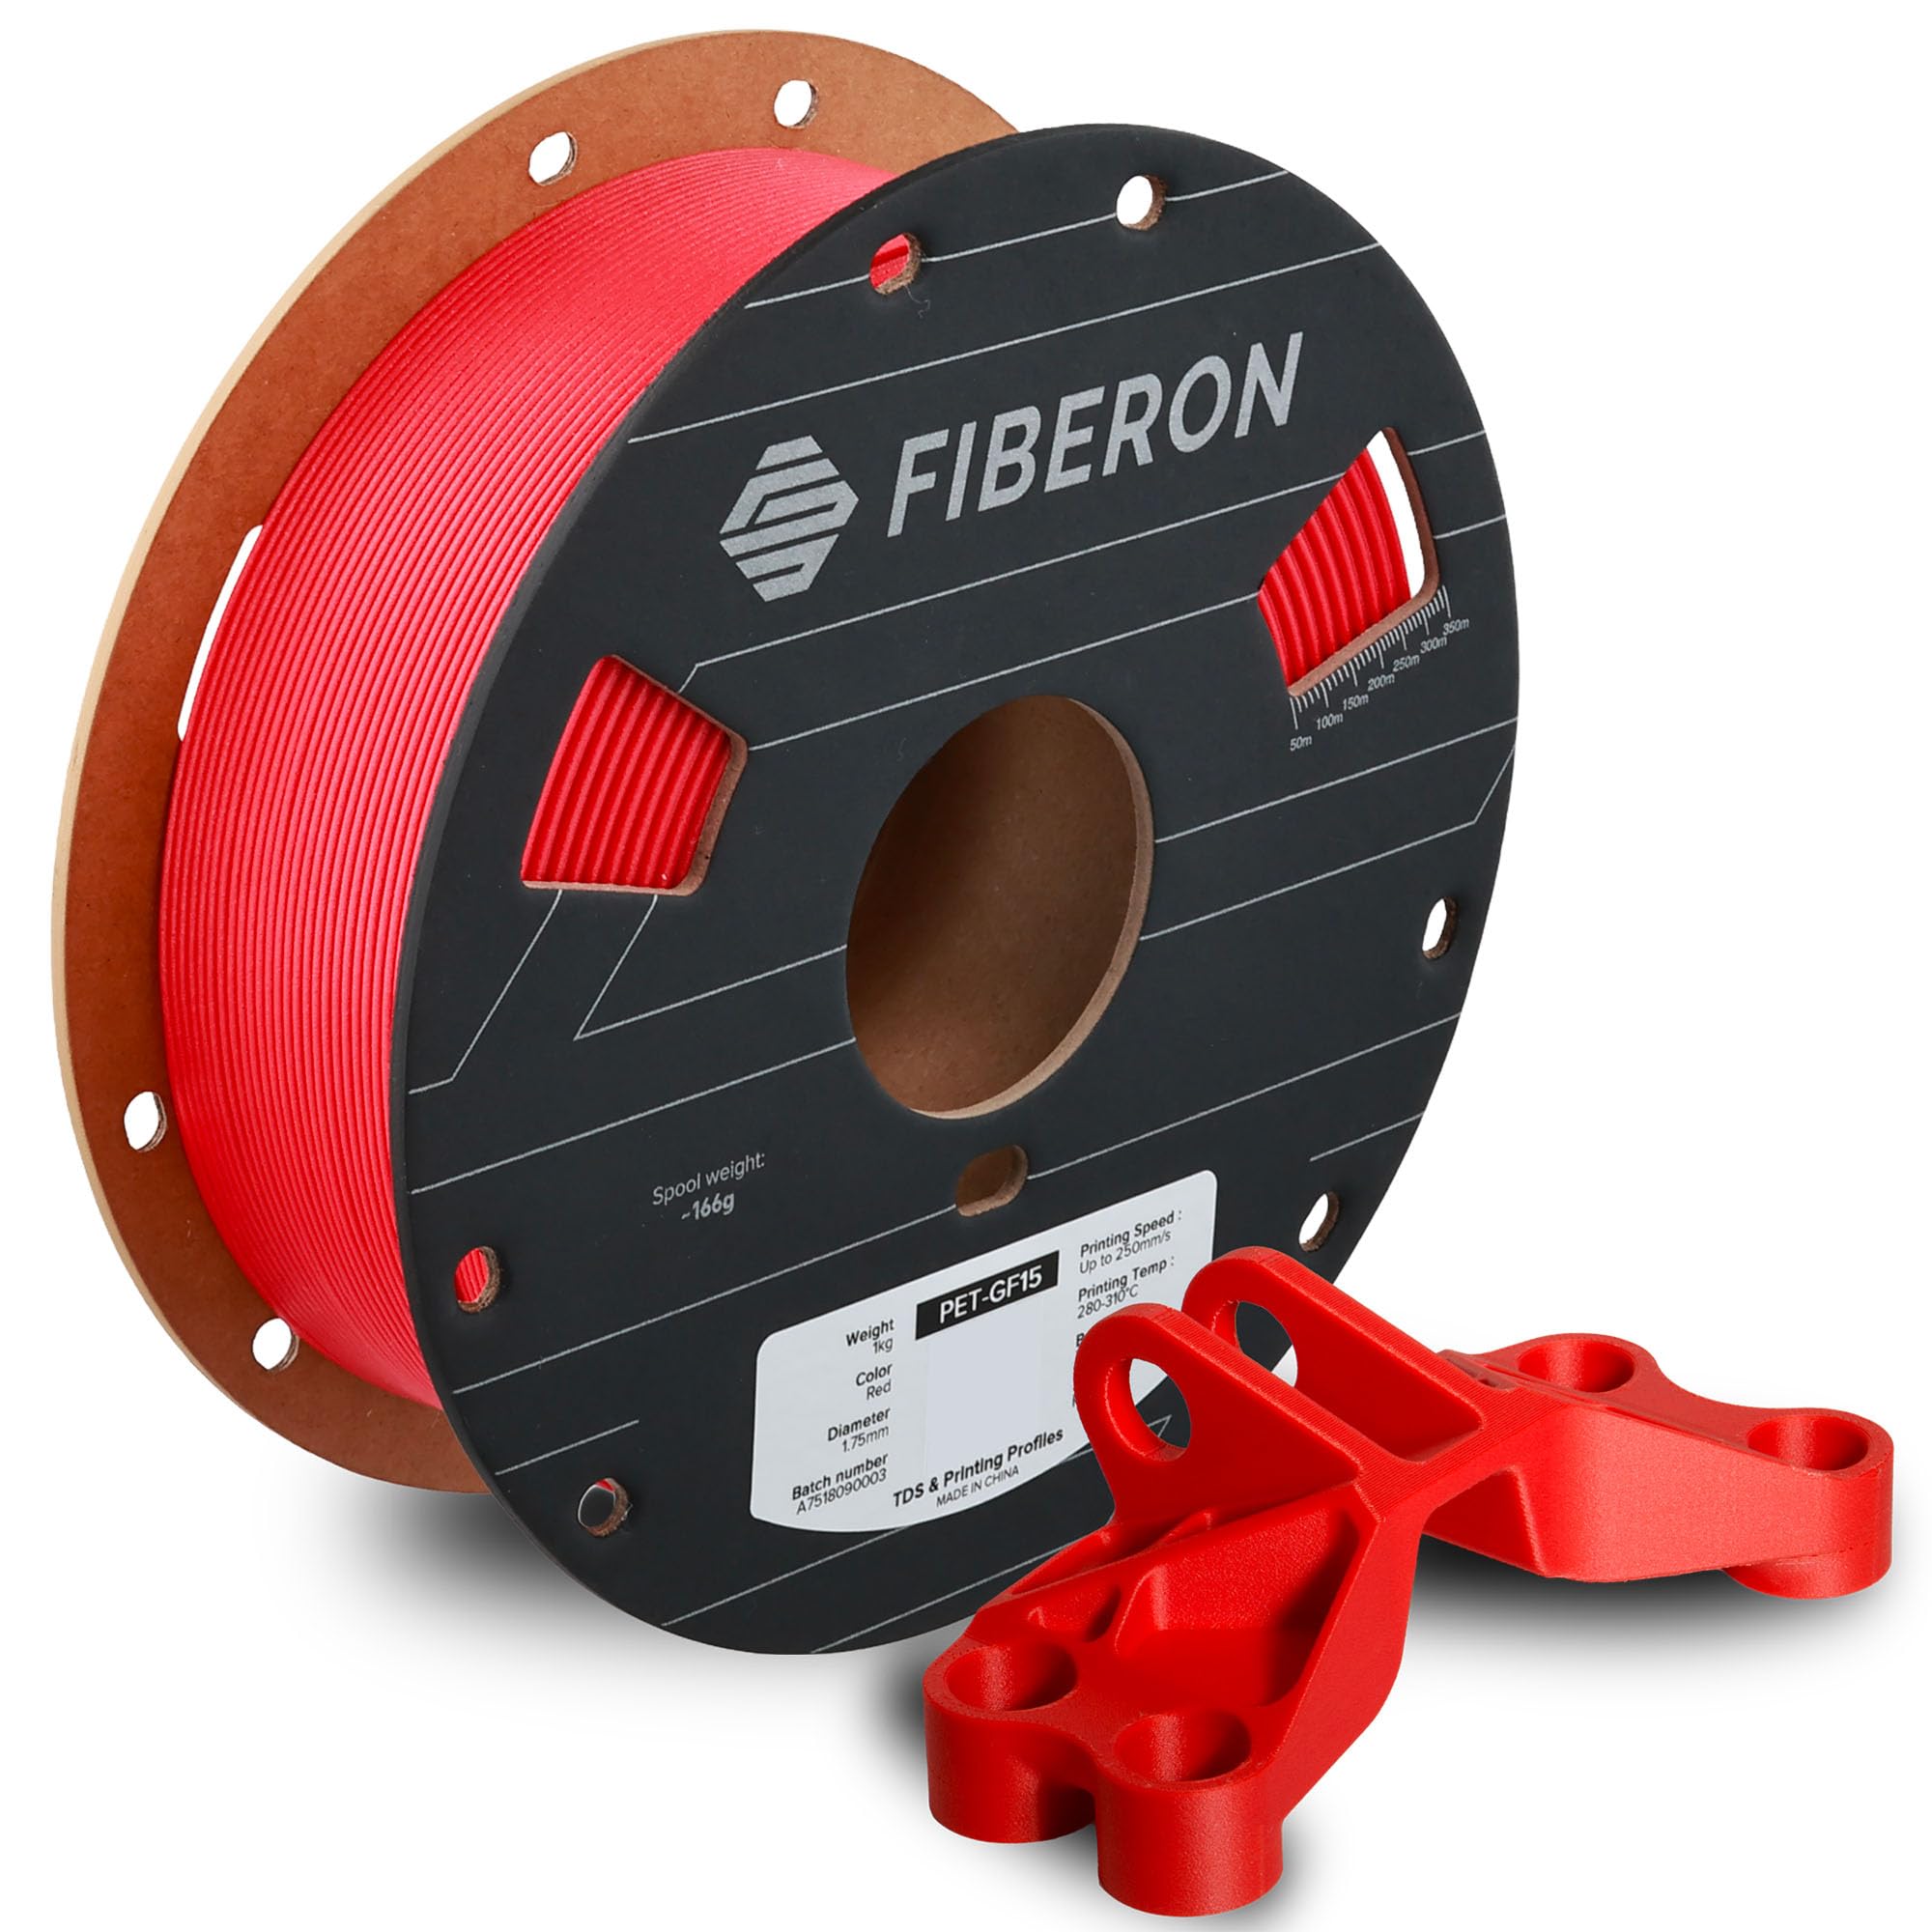
Polymaker Fiberon PET-GF15 Glass Fiber PET Filament 1.75mm, Red, 1kg | For rigid fixtures, brackets and heat-exposed parts; 15% glass fiber PET with($29.99Value)
$29.99
Polymaker Fiberon PET-GF15 Glass Fiber PET Filament 1.75mm, Red, 1kg | For rigid fixtures, brackets and heat-exposed parts; 15% glass fiber PET with($29.99Value)
Description
15% Glass Fiber Reinforced PET: Combines high strength, stiffness, toughness, and dimensional stability for functional prototypes, jigs, fixtures, brackets, enclosures, automotive components, and durable end-use parts. Annealed HDT up to 133.7°C: As-printed specimens reach an HDT of 81.6°C at 0.45 MPa. After annealing at 120°C for 16 hours, HDT increases to 133.7°C at 0.45 MPa. Actual performance depends on load, geometry, orientation, and processing conditions. Clean Surface for Functional Parts: Glass fiber reinforcement helps reduce warping and maintain part geometry while producing a refined surface with less visible fiber exposure. Available in multiple colors for functional and appearance-focused projects. Use a Hardened Nozzle: Print at 280–310°C with a 70–80°C build plate and the cooling fan off. A hardened steel, ruby, or other wear-resistant nozzle is required because glass fiber can rapidly wear standard brass nozzles. Printing speeds up to 250mm/s are possible after calibration. Keep the Filament Dry: Store and print below 20% relative humidity. If moisture has been absorbed, dry at 100°C for 10 hours. An enclosed printer is recommended for tall or large parts, while smaller parts may be printed on an open-frame machine. Use supports during annealing when needed to reduce deformation. Polymaker Fiberon PET-GF15 is a 15% glass fiber-reinforced PET filament developed for strong, dimensionally stable, and heat-resistant functional parts. It combines stiffness, toughness, and a refined surface finish, making it suitable for jigs, fixtures, brackets, enclosures, functional prototypes, automotive components, and durable end-use parts. As-printed test specimens reach a heat deflection temperature of 81.6°C at 0.45 MPa. When additional heat resistance is required, printed parts may be annealed at 120°C for 16 hours, increasing the tested HDT to 133.7°C at 0.45 MPa. These values are material test results rather than continuous-use temperature ratings. Final performance depends on part geometry, wall thickness, load, print orientation, and processing conditions. For recommended results, print at 280–310°C with a 70–80°C build plate and the cooling fan off. A hardened steel, ruby, or other wear-resistant nozzle is required because glass fiber can rapidly wear standard brass nozzles. Printing speeds up to 250mm/s may be achieved after calibrating temperature, flow rate, layer adhesion, and machine motion settings. PET-GF15 is sensitive to moisture and should be stored and printed in dry conditions below 20% relative humidity. If the filament has absorbed moisture or produces stringing, bubbles, rough surfaces, or inconsistent extrusion, dry it at 100°C for 10 hours before use. An enclosed printer is recommended for tall or large parts to improve dimensional consistency. Smaller parts may be printed on an open-frame printer with the correct build plate temperature. PET-GF15 can bond strongly to textured PEI surfaces, so allow the plate to cool before removing the part or use a suitable release agent to help protect the build surface.
More Information
| Color | 117 - 1.75mm Fiberon Pet-gf15 Red 1kg (Hex Code: #Cc0033 |
| Size | PET |
| Gtin | 6938936716778 |
| Mpn | FL02007 |
| Age_group | ADULT |
| Condition | NEW |
| Gender | UNISEX |
| Material | Polyethylene Terephthalate |
| Product_category | Gl_biss |
| Google_product_category | Business & Industrial |
| Product_type | Industrial & Scientific > Additive Manufacturing Products > 3D Printing Supplies > 3D Printing Filament |